Quality & Certifications
Built on Documentation, Not Hope
Industrial Knives has run an ISO 9001:2015 quality system since 2001. Every blade we ship carries a documented chain from incoming steel to your dock —CMM report, mill certificate, hardness mapping and Cpk study on request.
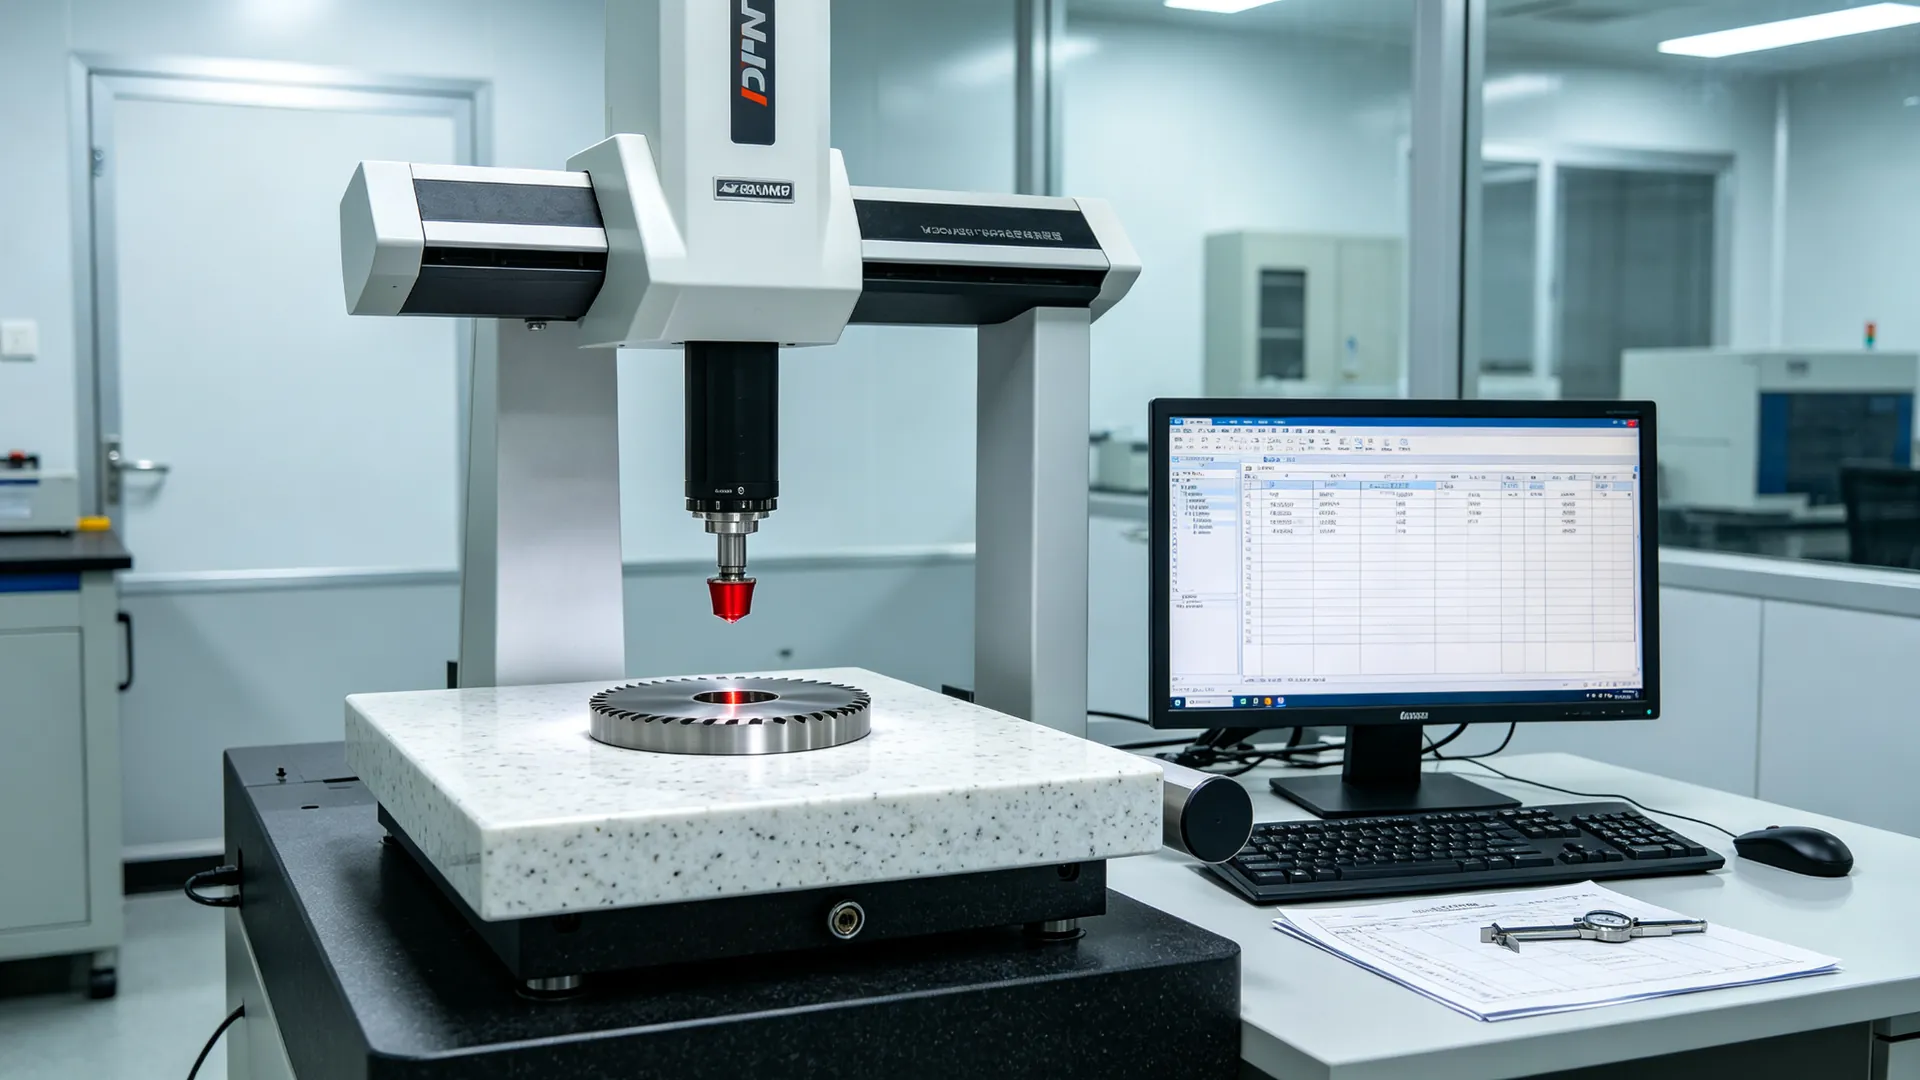
Looking for a blade supplier whose quality system you can actually audit? Most job shops will hand you a certificate they downloaded from the internet. We open our factory twice a month, walk you through incoming inspection, heat treatment, grinding, PVD coating and the quality lab, and answer any Cpk or PPAP question on the floor.
- —ISO 9001:2015 since 2001, surveillance audit 2026
- —EN 10204 3.1 mill certificate shipped with every batch
- —Cpk ≥ 1.33 on critical dimensions, quarterly audit
- —10-year document retention per ISO 9001 §7.5
- —No MOQ on prototype batches; pricing per drawing, no hidden fees
- —Engineering team response within one business day on every RFQ
Standards referenced
Six Standards That Govern Our Work
Every quote, every certificate and every inspection report maps to one of these published standards. We do not invent our own specification language.
Six published standards define how Industrial Knives specifies, inspects and certifies every blade. They are referenced on every quote and on every dispatch note —not as marketing language but as the actual numbers behind every claim.
Material grades cross-reference ASTM, DIN, JIS, GB and other national bodies. Surface finish and dimensional tolerances cite ISO 4287 / ISO 1101. Hardness testing follows ISO 6508. EN 10204 3.1 mill certificates ship with every production batch.
ISO 9001:2015
Quality management system certified since 2001. Surveillance audits every year. Last audit completed in 2026.
EN 10204 3.1
Mill Test Certificate type 3.1 with steel heat number. Shipped with every production batch.
ASTM A681 / DIN 1.2379 / JIS SKD11
D2 cold-work tool steel specified per ASTM A681, equivalent to DIN 1.2379 and JIS SKD11. Cross-reference on every quote.
Inspection lab
Six Instruments, Calibrated Daily
A short tour of the equipment that decides whether a blade ships or stays on the bench.
CMM (HEXAGON Global S)
Two coordinate measuring machines, including a HEXAGON Global S with ±0.003 mm repeatability. Every dimension on the customer drawing is measured, not just the ones that fit the schedule. Reports are signed off and shipped with the parts.
Rockwell Hardness Mapping
Three-point Rockwell C mapping on every blade, calibrated daily against a certified test block. Hardness survey attached to the CMM report. Out-of-spec hardness triggers a containment action and re-heat-treatment.
Surface Roughness (Ra)
Working edge: ≤Ra 0.2 µm. Ground surfaces: ≤Ra 0.8 µm. Measured on a contact profilometer, traced back to the grinding machine and operator. Flatness and parallelism verified on a granite plate.
Calotest Coating Thickness
PVD coating thickness measured on a Calotest ball-crater rig at two points per blade. TiN, TiCN, CrN and DLC coatings applied to ±2 µm uniformity in our two in-house PVD chambers.
Optical Comparator
Edge-profile and micro-geometry inspection on a 300 mm optical comparator with 10× magnification. Used for burr measurement (≥?50 µm target) and edge-prep land verification on thin-gauge substrate.
Micro-hardness Tester
Vickers and Knoop micro-hardness on the heat-affected zone, coating cross-section and weld repairs. Used to validate heat-treatment recipes on new steel grades before serial production.
Traceability chain
From Mill Heat to Shipped Blade
ISO 9001:2015 §8.5.2 requires identification of outputs throughout production. Our traveller links every stage back to the original steel heat number. The table below is the actual paperwork we generate.
| Stage | Artefact | Owner | Retention |
|---|---|---|---|
| Raw material | Mill Test Certificate per EN 10204 3.1 | IQC | 10 yr |
| Forging / rough machining | Heat number + rough-machining traveller | Production | 10 yr |
| Heat treatment | Furnace run record + hardness verification | Heat-treat | 10 yr |
| CNC grinding & EDM | In-process inspection + first-off CMM | IPQC | 10 yr |
| PVD coating | Coating batch + Calotest thickness | Coating | 10 yr |
| Final inspection | CMM report + Rockwell mapping + Ra report | FQC | 10 yr |
| Shipment | Packing list + CoC + customer-specific docs | OQC | 10 yr |
Standards referenced:ISO 9001:2015,EN 10204,ASTM A681.
Comparison
Industrial Knives QA vs Typical Job Shop
How our quality system compares to a typical CNC job shop. The differences show up in the paperwork that travels with every shipment.
| KPI | Industrial Knives | Typical Job Shop |
|---|---|---|
| ISO 9001:2015 certified | Yes, since 2001 | Varies; often not certified |
| Mill certificate per EN 10204 3.1 | Shipped with every batch | Only on request, surcharge |
| CMM inspection | Every dimension on drawing | Critical dims only |
| CMM repeatability | ±0.003 mm (HEXAGON Global S) | ±0.01 mm typical |
| Hardness mapping | 3-point Rockwell C per blade | Single spot check |
| Surface roughness on edge | ≤Ra 0.2 µm, profilometer | Visual, no instrument |
| Cpk on critical dims | ≥ 1.33, quarterly audit | Not tracked |
| PPAP / ISIR package | On request, AIAG-compliant | Not offered |
| Coating adhesion test | VDI 3198 per batch | Not tested |
| Document retention | 10 yr per ISO 9001 §7.5 | 1–7 yr |
| Customer audit support | On-site, twice monthly | By appointment, limited |
| NCR turnaround | 8D within 5 business days | Ad hoc |
FAQ in full
Detailed Q&A
Is Industrial Knives ISO 9001 certified, and how long has the certificate been valid?
Yes. Industrial Knives has held ISO 9001:2015 certification continuously since 2001, with the most recent surveillance audit completed in 2026. The certificate, quality manual and a sample CMM inspection report are available on request under NDA.
- ISO 9001:2015 certified since 2001
- Surveillance audit: 2026
- AS9100 readiness in progress for aerospace customers
- Quality manual and sample CMM report available on request
What traceability chain links a finished blade back to its raw material?
Every finished blade carries a heat number that traces all the way back to the mill heat. ISO 9001:2015 §8.5.2 requires identification of outputs throughout production, and our system enforces it on every batch.
- Incoming steel: mill certificate per EN 10204 3.1 with heat number
- Heat-treatment batch record with furnace run ID
- Grinding and edge-prep traveller linked to the heat-treatment batch
- Final CMM and hardness report archived against the blade serial
Do you provide PPAP and ISIR packages?
Yes. We supply PPAP level 3 and full ISIR (Initial Sample Inspection Report) packages on request for automotive and Tier-1 customers. The default package includes dimensional, material, hardness and coating evidence.
- PPAP level 3 with full dimensional layout
- ISIR with material cert and mechanical test results
- Cpk study on critical dimensions when serial production is planned
- AIAG-compliant format or customer template
How is Cpk ≥ 1.33 calculated and audited?
Cpk is computed against the customer drawing tolerance on a minimum of 25 consecutive parts. Our internal audit re-runs the calculation every quarter on running production. A Cpk below 1.33 triggers a containment action and a process review.
- Sample size: 25 consecutive parts minimum
- Tolerance: customer drawing callout
- Audit cadence: quarterly per dimension
- Trigger: containment + 8D if Cpk falls below 1.33
How are non-conforming parts handled?
Non-conforming parts are physically segregated in a locked NCR cage, logged in the corrective-action system, and dispositioned as scrap, rework, or use-as-is with engineering concession. Customers are notified in writing before any concession is shipped.
- Segregation: locked NCR cage with photo record
- Disposition: scrap, rework, or engineering concession
- Customer notification in writing before any concession
- 8D corrective action with root-cause analysis on every NCR
How long are quality records retained?
Quality records are retained for ten years per ISO 9001 §7.5. Mill certificates, CMM reports, hardness surveys and PVD batch records are archived digitally and indexed by blade serial number for the full retention period.
- Retention: 10 years per ISO 9001 §7.5
- Index: blade serial number
- Format: digitally signed PDF + raw CMM data
- Retrieval: typically within 2 business days
Do you accept third-party inspection?
Yes. We regularly host SGS, Bureau Veritas and customer-side inspection teams at our factory. Inspection windows are pre-arranged, the production batch is held, and the inspector is given full access to CMM reports, raw data and test certificates.
- Pre-arranged inspection window with production hold
- Full access to CMM data, certificates and travellers
- Standard hosts: SGS, Bureau Veritas, customer-side engineers
- Cost: no fee for routine surveillance; pre-quoted for witness testing
Can a customer audit the factory?
Yes. We host supplier audits on-site twice a month on average. A typical audit covers incoming inspection, heat treatment, grinding, PVD coating and the quality lab. We share the audit checklist in advance and assign a quality engineer to escort the auditor for the full day.
- Frequency: ~2 on-site audits per month
- Coverage: incoming → heat treatment → grinding → PVD → QA lab
- Checklist shared in advance
- Dedicated quality engineer escort for the full day